Production Problems It Solves
Dust released at repeated open transfers
Chain-mounted discs carry material inside a tube, reducing open carrying surfaces between connected machines. Inlet and outlet containment still matter.
Equipment separated by levels or obstacles
One engineered circuit can combine level runs, vertical lifts and bends instead of requiring a separate transfer machine at every change of direction.
Where It Fits in Your Plant
Chemical batching
Transfer dry calcium carbonate, soda ash or compatible additives from a feed hopper to a mixer. Cohesion, corrosion and residue at outlets determine the contact materials and cleanout arrangement.
Ingredient and pellet handling
Connect flour handling or plastic-pellet storage to a receiving hopper. Cleaning access matters for recipe changes; fragile products need breakage checks under the selected speed and route.
How the Pipe Chain Conveyor Works
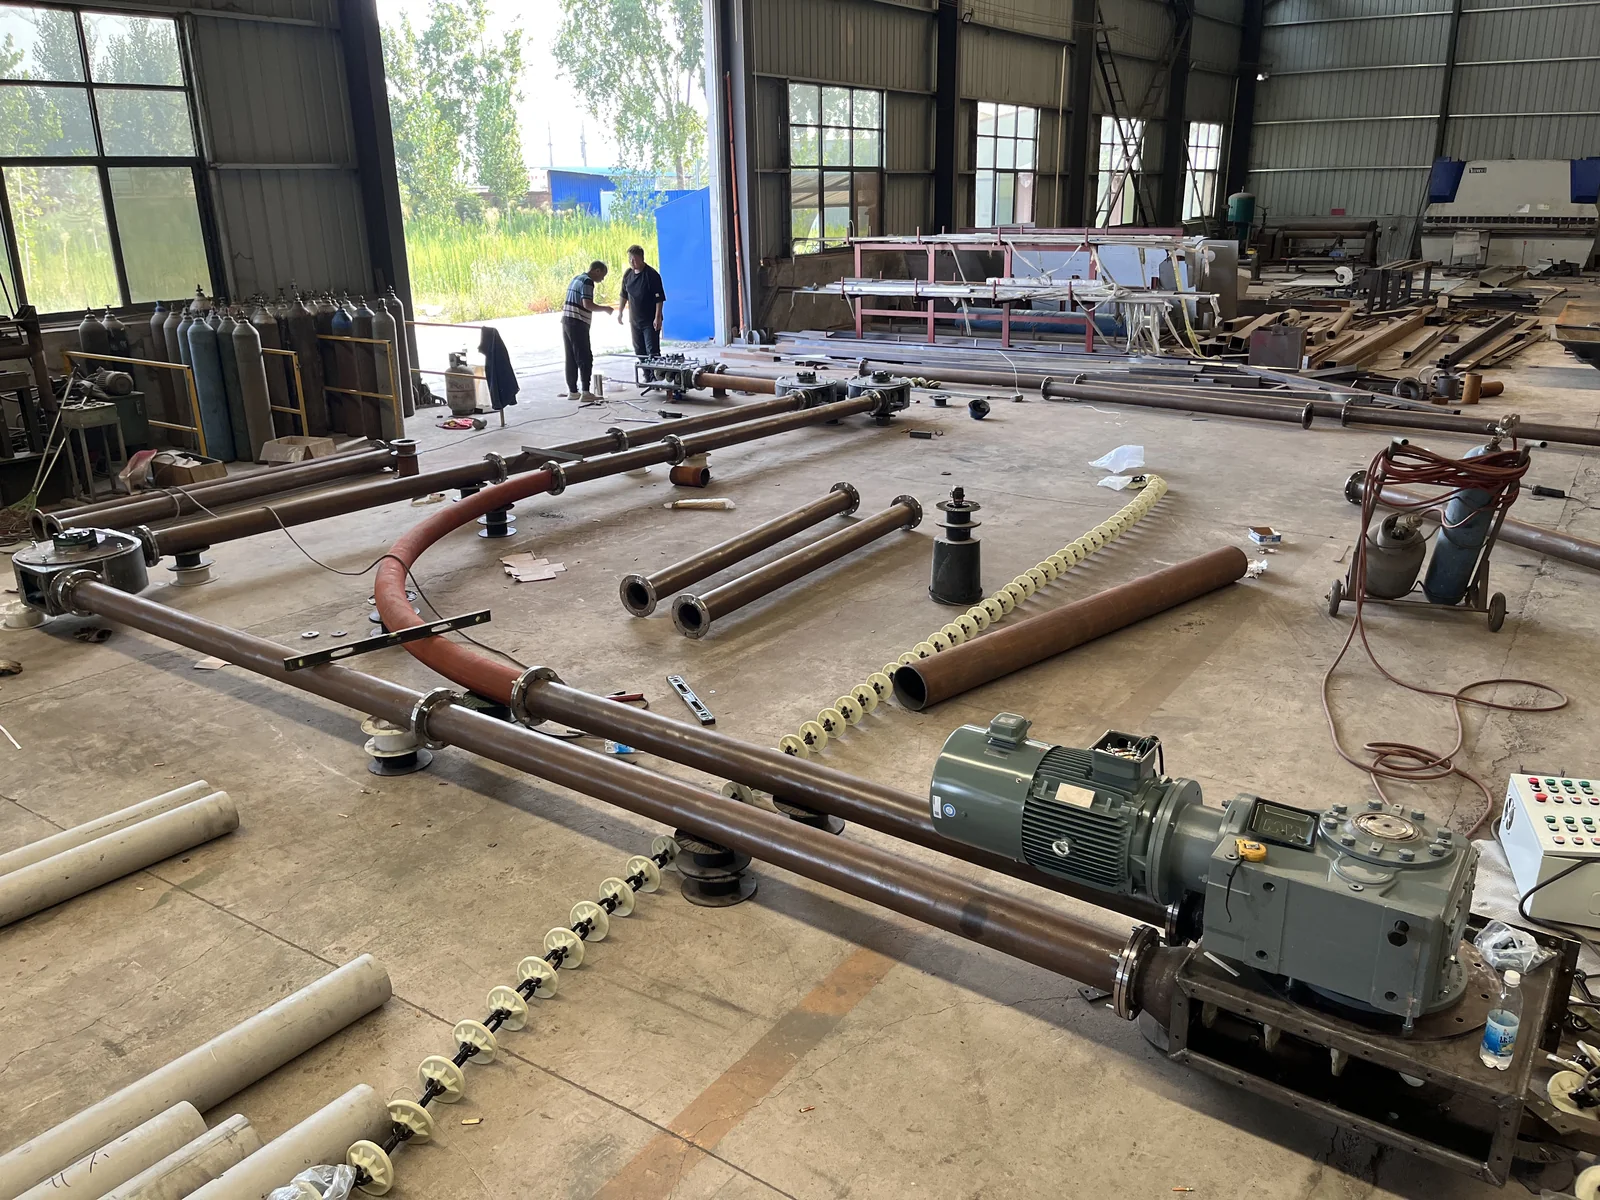
The drive moves chain-mounted discs through a closed tube circuit. In horizontal runs the discs push material as a bulk mass; in vertical runs they support and lift it. Large-radius bends change direction, and the return tube brings the chain back through the circuit. Drive loading depends on the complete route, material density and filling condition.
Selection Factors
- Complete circuit: include both the loaded run and return path when assessing length, resistance and service access.
- Throughput: tube fill and chain speed govern volume flow; mass flow also depends on loose bulk density.
- Cleanout: place accessible inspection points at receivers, bends and areas where residual product can collect.
Suitable Materials for Conveying
The examples below describe dry-solid conveying duties. Powder grade, moisture, contact materials and route loading determine the required configuration. Food and chemical duties need different contact and cleaning arrangements.
Chemical powders & additives 3 examples
Sodium bicarbonate & soda ash
- Material form
- Dry carbonate powders or crystals
- Typical application
- Transfer additives from storage or bag dumping to batching and mixing
- Handling considerations
- Keep moisture out of the inlet; hard lumps can restrict pickup. Select seals and contact surfaces for the actual chemical grade and cleaning method.
Titanium dioxide & iron oxide pigments
- Material form
- Fine pigment powders
- Typical application
- Enclosed transfer to powder blending, coatings or pigment batching
- Handling considerations
- Fine dust requires sealed feed and receiver connections. Retained pigment at outlets and bends can carry colour into the next batch; provide accessible cleanout points.
Detergent granules & sodium phosphate
- Material form
- Dry formulated granules or chemical powders
- Typical application
- Connect ingredient storage, blending and packaging receivers
- Handling considerations
- Cohesive grades can bridge at the feed hopper. Product temperature and chemical contact govern seal and disc compatibility; enclosure does not remove inlet bridging.
Mineral fillers & building materials 2 examples
Calcium carbonate, talc, kaolin & bentonite
- Material form
- Dry mineral filler powders
- Typical application
- Supply filler powders to mixing and batching equipment
- Handling considerations
- Different powder grades have different bulk density and cohesion. Use controlled inlet loading; inspect dust seals, deposits and wear at bends rather than assigning one rate to every filler.
Cement & dry mineral powder
- Material form
- Dry building-material powders
- Typical application
- Transfer bulk ingredients between storage, mixers and packing equipment
- Handling considerations
- Exclude wet lumps from the pickup. Abrasion and compacted residues affect the chain, discs and tube; access to the outlet and low points is needed for cleanout.
Plastics & resins 2 examples
PET & other plastic pellets
- Material form
- Free-flowing polymer pellets
- Typical application
- Connect pellet storage to blending or receiving hoppers
- Handling considerations
- Match disc clearance and inlet loading to pellet size. Bends can generate fines; keep grade-change residues out of the next pellet batch.
PVC & other resin powders
- Material form
- Dry polymer powders
- Typical application
- Supply resin powder to blending and dosing equipment
- Handling considerations
- Fine powder needs sealed connections and accessible residue removal. Cohesion, static behaviour and the product contact requirements determine the configured duty.
Grain & food ingredients 2 examples
Wheat, rice & corn
- Material form
- Dry cereal grains
- Typical application
- Move grain between storage, cleaning, blending and receiving equipment
- Handling considerations
- Foreign objects can interfere with discs and outlets. Control inlet loading and bend contact to limit broken grain; residual grain affects batch separation.
Flour, starch, sugar & salt
- Material form
- Dry ingredient powders or crystals
- Typical application
- Connect ingredient storage to mixing and packaging
- Handling considerations
- Keep ingredient-contact surfaces accessible for cleaning. Flour and starch deposits differ from sugar or salt crystals; moisture, corrosion and crystal breakage require material-specific choices.
Feed & fertilizer materials 2 examples
Animal feed pellets & dry feed ingredients
- Material form
- Formed feed pellets or dry ingredient particles
- Typical application
- Transfer feed ingredients and pellets to blending or packing receivers
- Handling considerations
- Pellet friability and powder carryover affect usable output. Plan emptying and cleaning between formulations; a dust-tight tube alone does not prevent cross-contamination.
Urea & fertilizer granules
- Material form
- Dry prills or formed fertilizer granules
- Typical application
- Connect dry-product storage, blending and packing equipment
- Handling considerations
- Moisture-related caking can obstruct the inlet. Limit impact at bends and discharge points to reduce new fines; contact-material compatibility follows the formulation.
Adsorbents & process additives 1 examples
Activated carbon powder & granules
- Material form
- Fine carbon powder or friable granules
- Typical application
- Move adsorbent from storage to a dosing or receiving point
- Handling considerations
- Powder containment and granule breakage are separate duties. Keep residues accessible for removal; dust properties and area classification determine any required protection measures.
Material Behaviour and Circuit Loading
Evaluate the loaded and return runs as one circuit. Moisture, bulk density, cohesion and bend contact determine the configured material duty.
Chemical Powder Conveying: What Changes the Duty
- Dust and colour carryover: seal the inlet and receiver, and keep outlet faces and bends accessible for residue removal. A closed tube does not eliminate pigment remaining from an earlier batch.
- Caking and bridging: moisture or cohesive powder can interrupt supply above the conveying inlet. Control hopper discharge before treating every low-flow problem as a drive problem.
- Contact compatibility: tube, chain, discs and seals all contact the product. Select their materials for the chemical grade, temperature and cleaning exposure; stainless steel alone does not establish compatibility with every chemical.
Technical Specifications
LIYOU catalogue specifications| Model | Tube outside diameter (mm) | Catalogue capacity (m³/h) | Fill factor | Maximum horizontal distance (m) | Maximum vertical lift (m) | Motor power range (kW) |
|---|
| GL89 | 89 | 3 | 0.5 | 45 | 15 | 1.1–11 |
| GL108/133 | 108 | 5–7 | 0.5 | 60 | 20 | 3–15 |
| GL159 | 159 | 10 | 0.5 | 60 | 30 | 3–22 |
| GL219 | 219 | 17 | 0.5 | 60 | 35 | 5.5–28 |
| GL273 | 273 | 30 | 0.5 | 60 | 45 | 5.5–30 |
| GL325 | 325 | 50 | 0.5 | 60 | 45 | 5.5–30 |
Catalogue reference conditions: material bulk density 1 t/m³; chain speed 0.3 m/s; fill factor 0.5; conventional dry powders. Capacity is stated as volume flow, not a material-independent mass rate. Maximum distance, lift and motor-power ranges describe catalogue options; the complete route and material determine the configured duty. The source groups GL108/133 in one row and lists tube OD Φ108 for that row.
GL-series capacity and parameter explanation
Common Issues & Checks
- Increasing drive load: inspect excessive feed, compacted material and wear at bends after safe isolation.
- Product carryover between batches: inspect outlet emptying and retained material in the circuit; enclosure alone does not eliminate residues.
Pipe Chain Conveyor Layouts
Related equipment
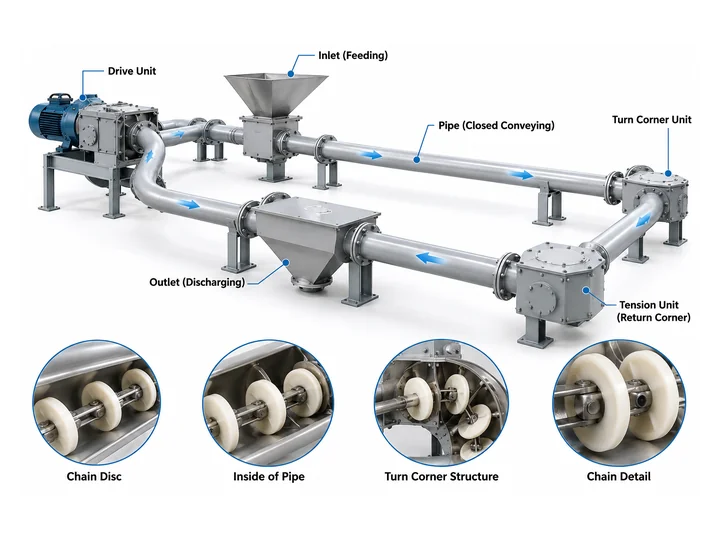
Connect hoppers, mixers and packing stations at similar elevations with a horizontal pipe chain conveyor for enclosed powder and granule transfer.
Explore equipment ↗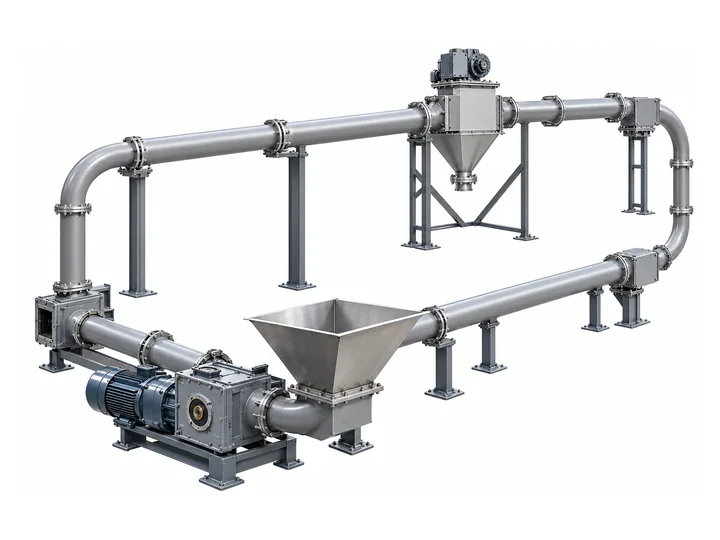
Lift dry powders and granules to upper hoppers with a vertical pipe chain conveyor using chain-mounted discs inside a tube.
Explore equipment ↗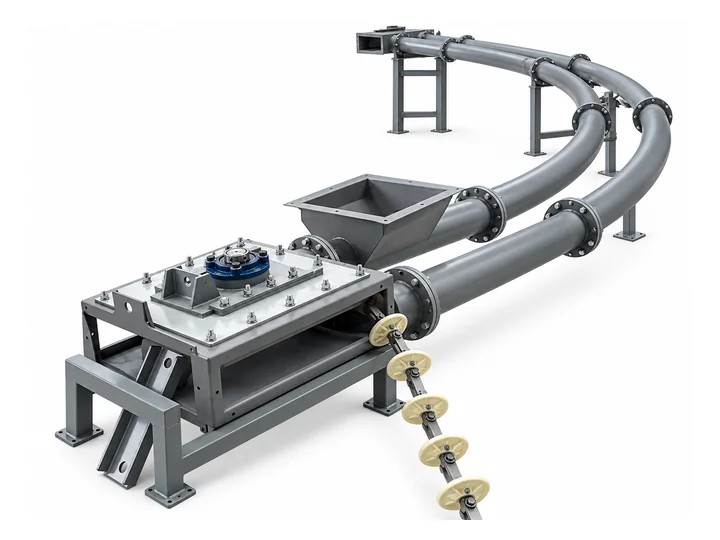
Route dry powders and granules around fixed plant equipment with a curved pipe chain conveyor using engineered tube bends.
Explore equipment ↗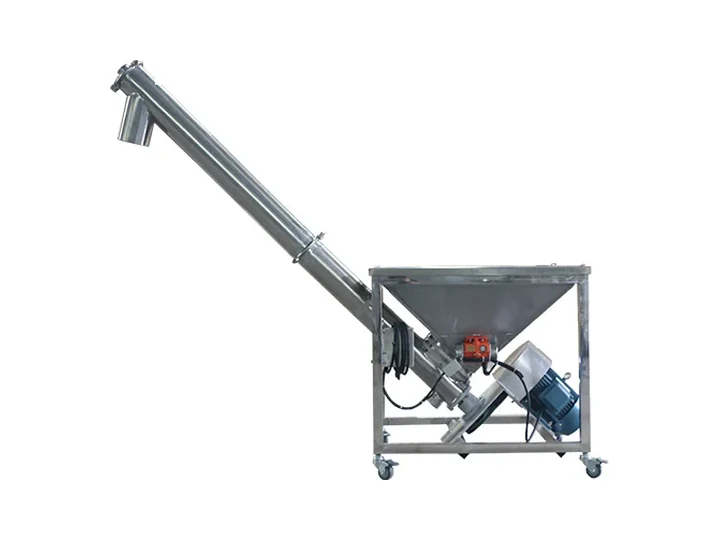
Transfer dry powders and granules between hoppers, mixers and packing equipment with a screw conveyor sized for the feed and incline.
Explore equipment ↗Related solutions
Screen calcium carbonate, resin and pigment powders; control agglomerates, mesh blinding and dust at enclosed transfer points.
View solution ↗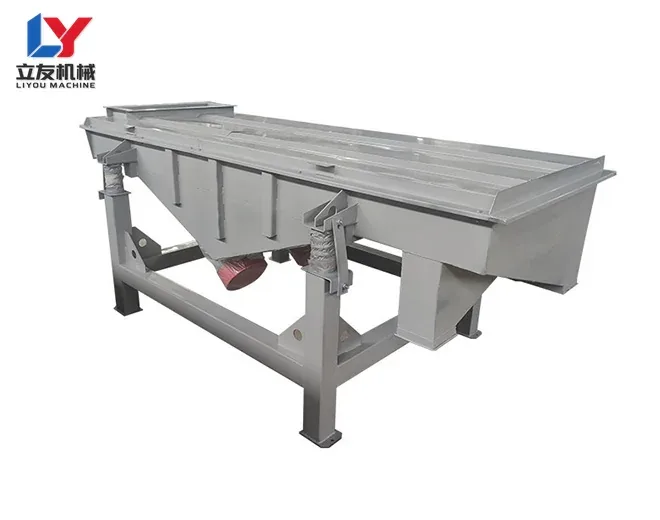
Polymer pellets require removal of off-size material and transfer to a receiving bin.
View solution ↗Technical resources
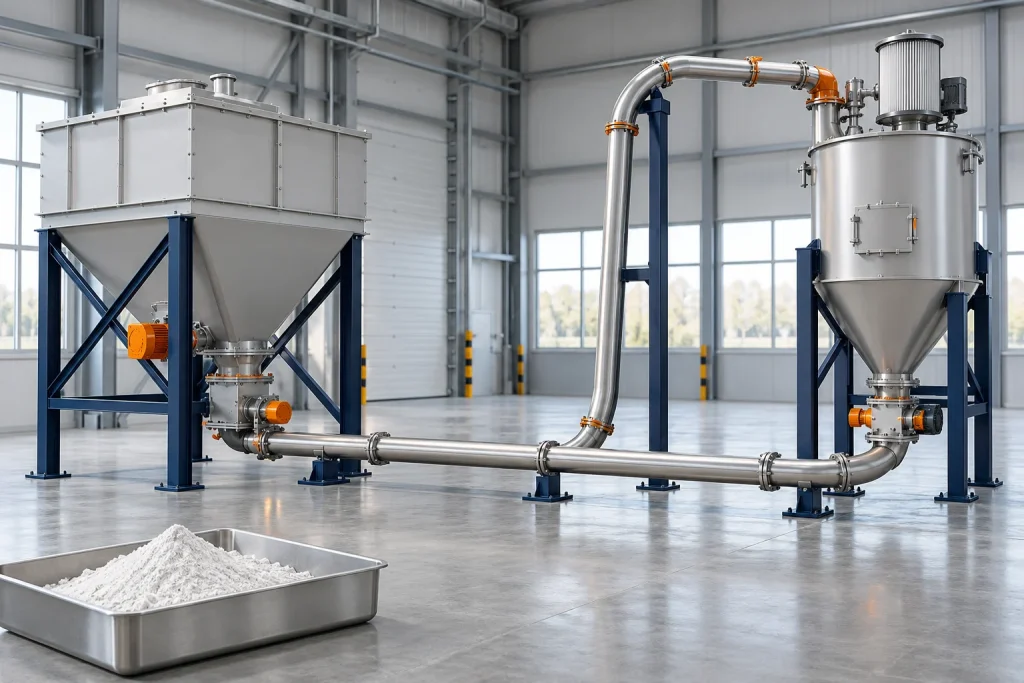
Application concept
Where dust escapes from enclosed powder conveyors, how retained powder causes carryover, and why abrasive fillers need wear inspection.
Read guide ↗
Powder conveying selection depends on more than distance.
Read guide ↗A tubular chain conveyor uses discs carried by a chain.
Read guide ↗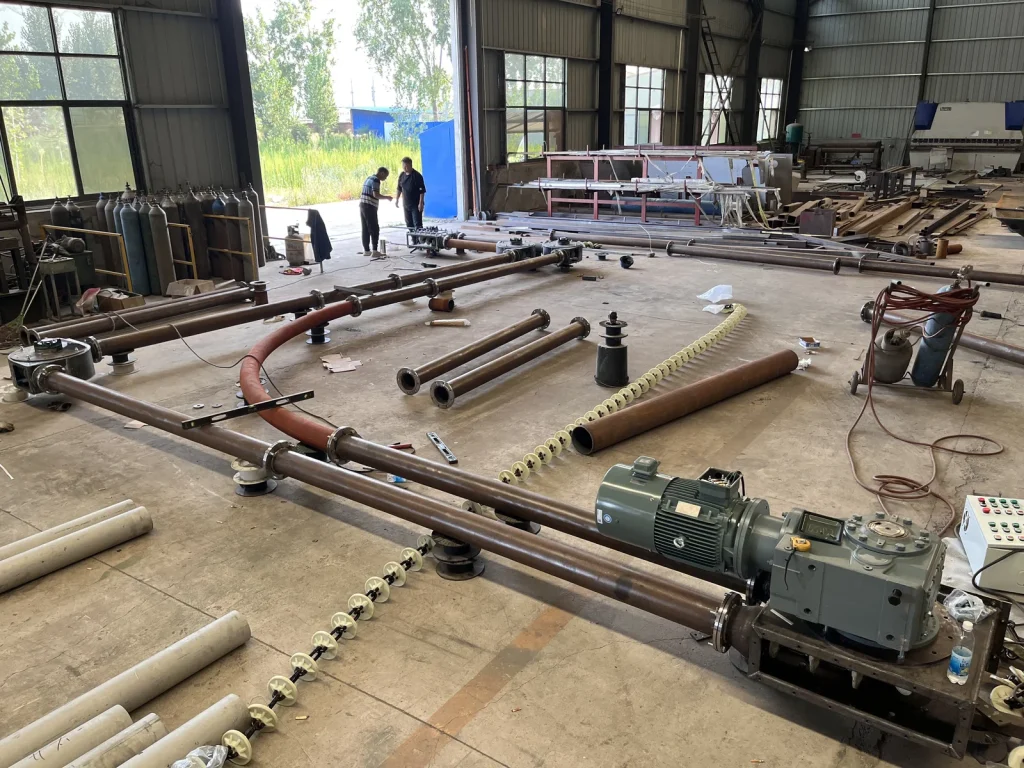
How tubular chain conveyors handle chemical powders, mineral fillers, resins, grains and ingredients, with practical dust, wear and cleanout conditions.
Read guide ↗Useful answers
Frequently asked questions
Is a pipe chain conveyor the same as a tubular screw?
No. Discs carried by a chain move the product rather than a rotating screw flight.
Can catalog cubic metres per hour be treated as tonnes per hour?
Only after applying the actual bulk density and evaluating the specified duty.